How to select plastic resins by melt flow rate for injection molding
Two resin grades can show the same melt flow rate and still behave differently in an injection mold. One may fill a thin rib cleanly; another may require more pressure or produce a weaker weld line. Selecting plastic resins by melt flow rate therefore starts with understanding what the number measures—and where its usefulness ends.
For technical evaluators, melt flow rate is a practical screening tool, not a complete material specification. A sound selection connects comparable test data with part geometry, mechanical requirements, machine capability, and evidence from molding trials.
Read the test conditions before comparing the numbers
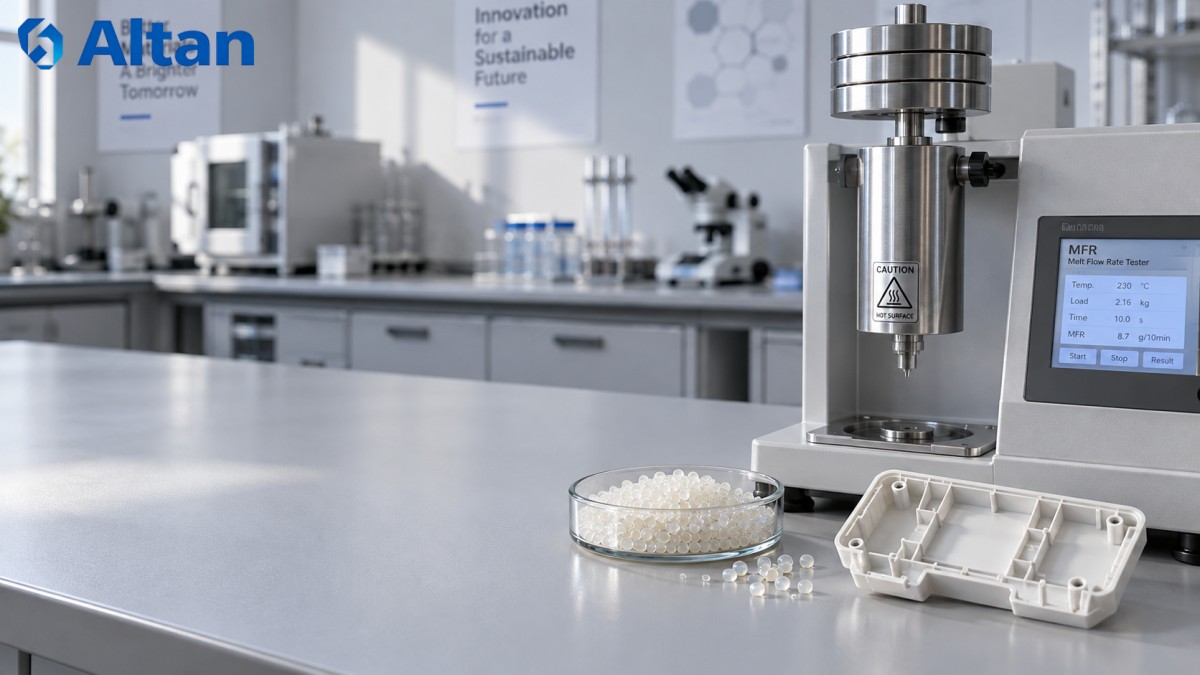
Melt flow rate (MFR), sometimes called melt flow index (MFI), expresses the mass of molten polymer passing through a standardized die over a specified time, typically reported in g/10 min. Common test methods include ASTM D1238 and ISO 1133.
An MFR value is meaningful only alongside its test temperature and load. For example, polypropylene data are commonly reported at 230°C/2.16 kg, while polyethylene data often use 190°C/2.16 kg. Comparing those numbers directly does not establish which material will fill your mold more easily.
Before ranking candidate grades, check:
- Polymer family and formulation: compare like-for-like materials wherever possible, including reinforcement and filler content.
- Temperature, load, and method: confirm that the reported values use equivalent conditions and compatible procedures.
- Measurement type: melt volume-flow rate (MVR), reported in cm³/10 min, is not interchangeable with MFR without the relevant melt-density information.
- Sample preparation: drying and conditioning matter, particularly for moisture-sensitive polymers.
A technical data sheet usually reports a typical value, not necessarily a guaranteed acceptance limit. Ask which specification controls shipment quality before turning a screening number into a purchasing requirement.
Match flow to the part—not simply to the highest available MFR
Within a comparable resin family, higher MFR generally indicates lower viscosity under the test conditions. That may help with long flow paths and thin sections. However, injection molding operates across a much broader range of shear rates than a standard melt-flow test, so the ranking does not fully describe cavity-filling behavior.
Consider the complete flow path: gate size, minimum wall thickness, ribs, changes in section, and the distance to the last point of fill. A short shot may reflect an undersized gate, trapped air, or insufficient machine capacity rather than an unsuitable resin grade.
Understand the performance trade-off behind higher flow
For otherwise similar polymers, higher MFR often corresponds to lower molecular weight. Easier flow can therefore come with reduced toughness, melt strength, or long-term performance. This is a tendency, not a universal rule: molecular-weight distribution, copolymer structure, modifiers, and fillers can change the relationship substantially.
That distinction matters when evaluating plastic resins for demanding components. A high-flow impact-modified grade may outperform an unmodified grade in impact testing, even when a simple MFR comparison suggests otherwise. Evaluate measured properties rather than assuming that flow alone predicts strength.
Moisture introduces another trap. In polymers susceptible to hydrolytic degradation, inadequate drying can increase apparent flow while damaging molecular chains. Easier filling under those circumstances is a warning, not an improvement. Confirm drying requirements, residual-moisture limits, and allowable residence time.
Build a shortlist that can survive a molding trial
Set non-negotiable requirements first: service temperature, chemical exposure, impact resistance, stiffness, dimensional tolerances, and any applicable regulatory requirements. Then use MFR to narrow the grades that meet those requirements and appear compatible with the tool.
For the finalists, request viscosity-versus-shear-rate data at relevant processing temperatures, recommended molding conditions, shrinkage data, and mechanical test details. For difficult geometries, mold-filling simulation can support the decision, provided the material model and process assumptions are appropriate.
During trials, record fill pressure, part weight, cycle time, flash, short shots, warpage, and critical dimensions. Test finished parts where weld lines, orientation, or conditioning may affect performance. The preferred grade should offer a workable processing window, not merely one successful shot.
Turn the selection into a controlled supply specification
Before approval, agree on the grade identity, MFR test conditions, acceptable range, lot traceability, and required shipment documentation. Where relevant, define limits for moisture, filler content, or recycled content separately; MFR cannot verify composition.
When sourcing through Shandong Qilun Chemical, provide the application requirements and agreed test criteria alongside the requested grade. This gives the sourcing discussion a clearer technical basis. The objective is not the highest MFR: it is a resin that fills the tool reliably, meets part-performance requirements, and can be evaluated consistently from shipment to shipment.
Related Posts
- ▶ How to select plastic resins by melt flow rate for injection molding
- ▶ Is potassium sulfate worth the premium over potassium chloride?
- ▶ How to prevent caustic soda crystallization in storage tanks
- ▶ Choosing an NPK Fertilizer Ratio Based on Soil Tests and Crop Needs
- ▶ How to Reduce Ammonia Loss When Applying Urea to the Soil Surface
- ▶ Potassium Sulfate in Fertigation: Solubility and Calcium Compatibility
Send Us A Message